
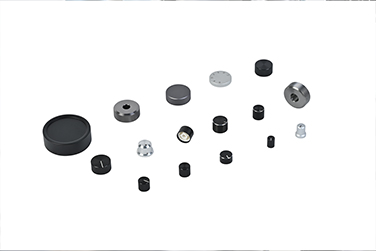
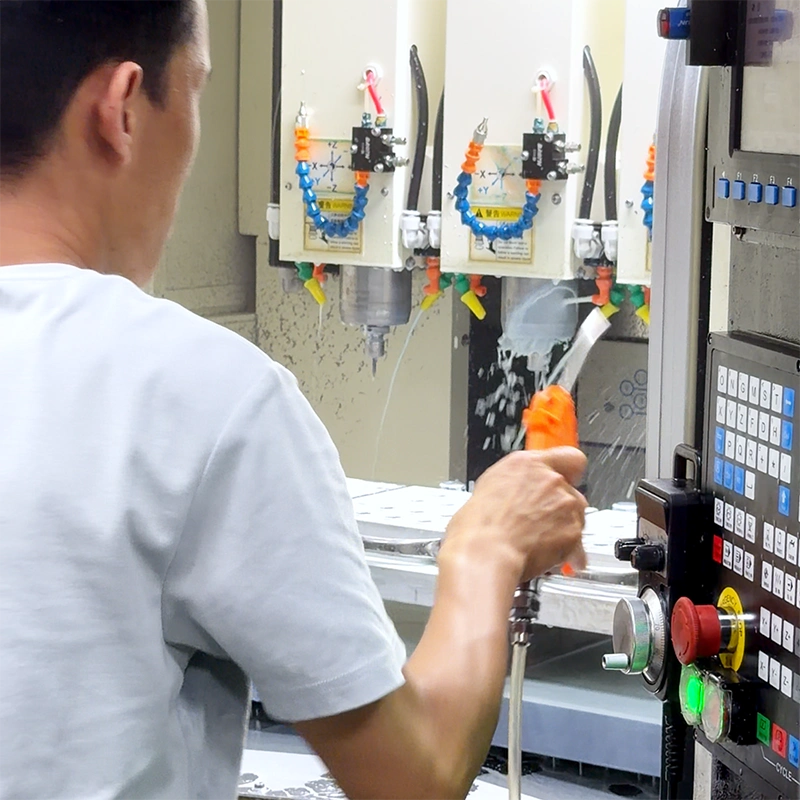
Small turned parts are not simply scaled-down versions of large ones. Once the diameter drops below about Ø10 mm and the length-to-diameter ratio passes 3:1, a fixed-headstock lathe starts to lose the argument: the tool pushes the bar away, chatter marks appear and the diameter drifts along the length. A Swiss-type lathe answers this with a guide bushing that supports the stock a fraction of a millimetre from the cutting edge, so the unsupported length stays close to zero however slender the part is. In practice the workable length-to-diameter ratio rises from about 3:1 to roughly 20:1.
小型车削件并不是把大零件等比例缩小。当直径降到约 Ø10mm 以下、长径比超过 3:1 时,固定主轴箱车床就开始力不从心:刀具把棒料推离,出现振纹,直径沿长度方向逐渐漂移。纵切(Swiss 型)车床用导套解决这个矛盾——导套在离切削刃不到一毫米的位置托住棒料,因此无论零件多细长,悬空长度都接近于零。实际可用的长径比也从约 3:1 提升到约 20:1。
That is how microscopic small turned parts get made repeatably: contacts and pins below Ø1 mm, ferrules, micro shafts and small threaded inserts. On our Swiss-type cells the diameter range runs 0.5–32 mm with a typical working window of 1–20 mm, diameters hold ±0.005–0.01 mm, roundness lands at 0.002–0.005 mm and the as-turned surface reaches Ra 0.4–0.8 µm. Live tooling on the same machine adds cross drilling, flats and slots, so a part that would otherwise need three setups comes off one machine complete, and concentricity between features turned in the same clamping stays inside 0.005–0.01 mm.
微观级小型车削件就是这样被稳定做出来的:Ø1mm 以下的触点与插针、套圈、微型轴和小螺纹嵌件。我们的纵切单元直径范围为 0.5–32mm(常用窗口 1–20mm),直径公差 ±0.005–0.01mm,圆度 0.002–0.005mm,车削表面粗糙度可达 Ra 0.4–0.8 µm。同一台机床上的动力刀具还能做横向钻孔、铣扁与铣槽,原本需要三次装夹的零件可以一次加工完成;同一次装夹车出的各特征之间,同轴度保持在 0.005–0.01mm 以内。
Swiss-type turning is not free. It is slower per part than a conventional lathe on a chunky component, and it only accepts bar, so anything above Ø32 mm or with a wide flange goes to a fixed-headstock machine that takes work up to Ø400 mm. We route on geometry rather than habit. If your drawing mixes a slender shaft with a wide flange, expect a two-machine route, and say so in the RFQ so the quote reflects the real process.
纵切加工不是没有代价的。对于粗壮的零件,它的单件节拍比普通车床慢,而且只吃棒料,因此直径超过 Ø32mm 或带宽法兰的零件要转到固定主轴箱机床上加工,那类设备最大可加工到 Ø400mm。我们按几何形状排产,而不是按习惯。如果你的图纸同时有细长轴和宽法兰,就应当预期两段式工艺,并在询价时说明,这样报价才能反映真实工序。